Drills
Solid carbide and through-coolant drills and modular drilling solutions for a wide range of diameters and depths.
Home / Drills
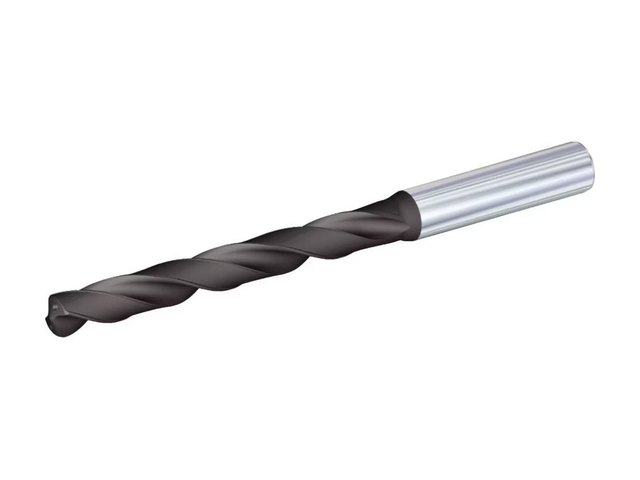
Drilling is one of the most frequent machining operations and often carries a part's most critical tolerances. The right drill determines hole quality, chip evacuation and cycle time.
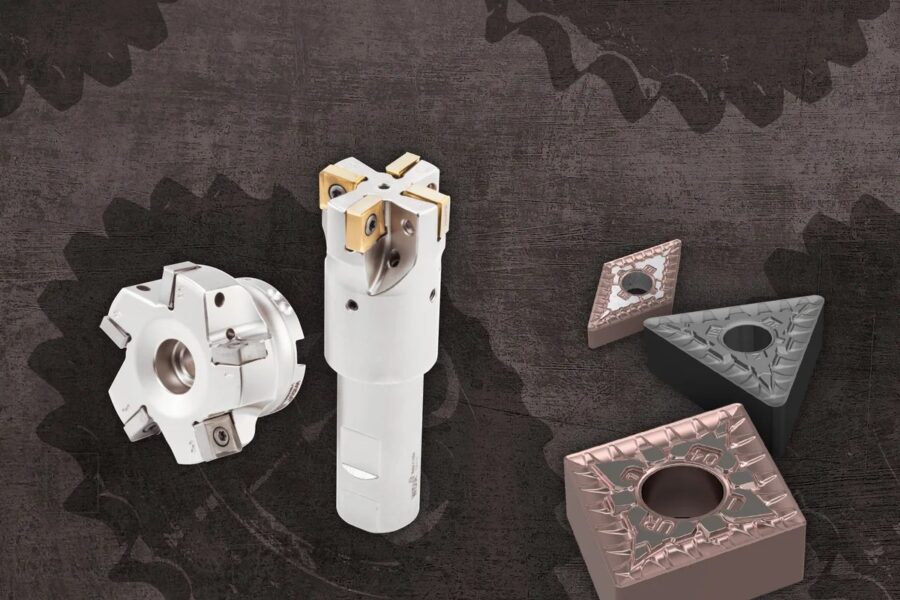
Techment offers WIDIA solid carbide drills, through-coolant drills and indexable/modular drilling systems, from small to large diameters and from shallow to deep holes. Together we define the most efficient drilling strategy for your diameter, depth, tolerance and material.
- Solid carbide, indexable and modular drilling systems
- Through-coolant designs for reliable chip evacuation in deep holes
- Geometry selection aimed at tolerance and surface finish
- Cutting data recommendations that shorten cycle time
Types of Drills
Solid Carbide Drills
High precision, good hole quality and high feed in small to medium diameters.
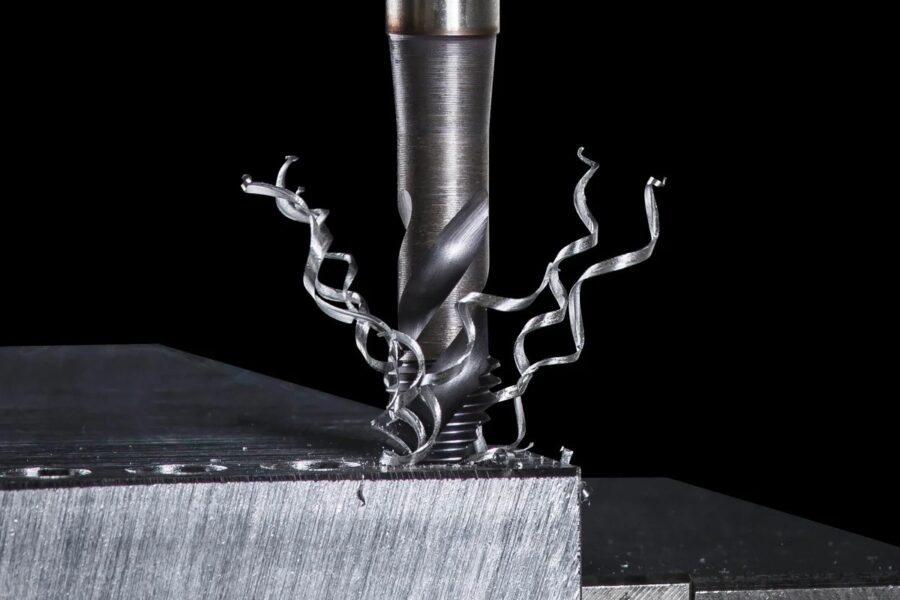
Through-Coolant Drills
Deliver coolant to the cutting zone, improving chip evacuation and tool life in deep holes.
Indexable Insert Drills
Economical drilling in large diameters: replace the worn insert, keep the body.
Modular / Replaceable-Tip Drills
Only the carbide tip is replaced while the body stays, cutting stock and cost.
Deep Hole Drills
For straight, precise holes several diameters deep.
Spot and Centre Drills
To locate the hole start and create a chamfer.
Applications
- Automotive blocks, heads and transmission housings
- Hydraulic and pneumatic manifolds
- Aerospace fastener holes
- Mold cooling channels
- General engineering
- Energy and defence components
Workpiece Materials
We offer suitable geometries and grades for every ISO material group.
- PSteel
- MStainless steel
- KCast iron
- NAluminium & non-ferrous
- SSuperalloys & titanium
- HHardened steel
How to Choose the Right Tool
Define the hole
Diameter, depth (L/D), tolerance and finish determine the drill type.
Define the material
ISO material group drives point angle, coating and flute design.
Consider coolant
Through-coolant availability and pressure are critical for chip evacuation in deep holes.
Check machine and holding
Spindle power, runout and rigidity directly affect hole quality and tool life.
Frequently Asked Questions
When do I need a through-coolant drill?
Usually when hole depth exceeds 3–5 × diameter, or in difficult materials such as stainless steel and superalloys. It improves chip evacuation, reduces heat and extends tool life.
Solid carbide or indexable drill?
Solid carbide drills are best for small to medium diameters and tight tolerances. In large diameters, indexable drills lower tooling cost.
My hole tolerance is tight. Do I need a reamer?
High-quality carbide drills reach IT8–IT9 in many applications. Tighter tolerances may require reaming or hole finishing tools; we assess this for your part.
Why is my drill life short?
The most common causes are high runout, unsuitable speed/feed, insufficient coolant and chip packing. We can review your process to find the cause.